Guide · Desoldering
How to use solder wick
Step-by-step desoldering with copper braid: choose the width, add flux, heat through the braid and lift it with the iron, plus fixes when wick won't work.
We may earn a commission if you buy through links on this page, at no extra cost to you. Unless a page says otherwise, our picks come from published specifications and listing research, not hands-on testing. As an Amazon Associate I earn from qualifying purchases. How we make money · How we research
Short answer
Add flux, lay the braid flat on the solder, and press a hot, tinned tip on top of the braid. When the solder flows up into the copper, lift the braid and the iron away together, then cut off the used end. If the braid will not take solder, the fix is usually more flux, fresh braid or a bigger tip, not more pressure.
What solder wick is
Solder wick, also called desoldering braid, is braided thin copper wire that soaks up molten solder.[1] Most braid comes with dry flux already applied.[2] It works by capillary action: molten solder is drawn into the gaps between the copper strands.
Wick is the tool for flat jobs. For clearing leftover solder out of through-holes, SparkFun calls a solder vacuum a great tool.[1]
| Job | Reach for |
|---|---|
| Excess solder on a pad | Wick |
| A bridge between two pins | First drag a clean, hot tip between the pins; use wick if the bridge stays[3] |
| Leftover solder in a through-hole | A desoldering pump, then wick to tidy the pad |
| Leveling pads after removing a surface-mount part | Wick |
| Lifting a multi-pin surface-mount part | Hot air; see the hot-air station buying guide |
What you need
- Braid of the right width. Pick braid about as wide as the pad you are clearing. Too narrow and it takes many passes; too wide and it spreads the iron's heat over copper you do not need.
- Flux. A little liquid or paste flux on the joint helps even pre-fluxed braid. See rosin vs no-clean vs water-soluble flux.
- A tip with a flat face. A chisel, bevel or knife tip presses flat on the braid; a fine conical point touches it at one spot. Adafruit's Collin's Lab recommends a flat "screwdriver" tip for through-hole work and a fine point for very small surface-mount parts.[4]
- A sensible temperature. SparkFun teaches a medium heat of 325-375 °C for learning.[5] Adafruit suggests 370 °C for 60/40 solder and 400 °C for lead-free, and notes that lead-free solder may need more heat and more flux.[6]
- Flush cutters to trim used braid, and isopropyl alcohol if you clean off flux residue.
For braid and flux, MG Chemicals' 424-NS is a #2-width no-clean braid, and Chip Quik's CQ4LF is a no-clean flux pen that puts a thin line of flux on the joint. A no-clean residue can stay on the board.[1]
If your station takes C245 cartridges and you only have a fine conical tip, a knife-shaped cartridge gives the braid a flat face to sit under. See T12 or C245 tips if you are not sure which system you have.
Step by step
- Heat and tin the iron. Bring it to temperature and tin the tip with a little fresh solder so heat transfers well. SparkFun tins the tip before each joint.[5]
- Flux the joint. Put a small amount of flux on the solder you want to remove.
- Place fresh braid. Lay a clean, unused section flat across the solder. Hold it by the spool or the long end, not near the joint.
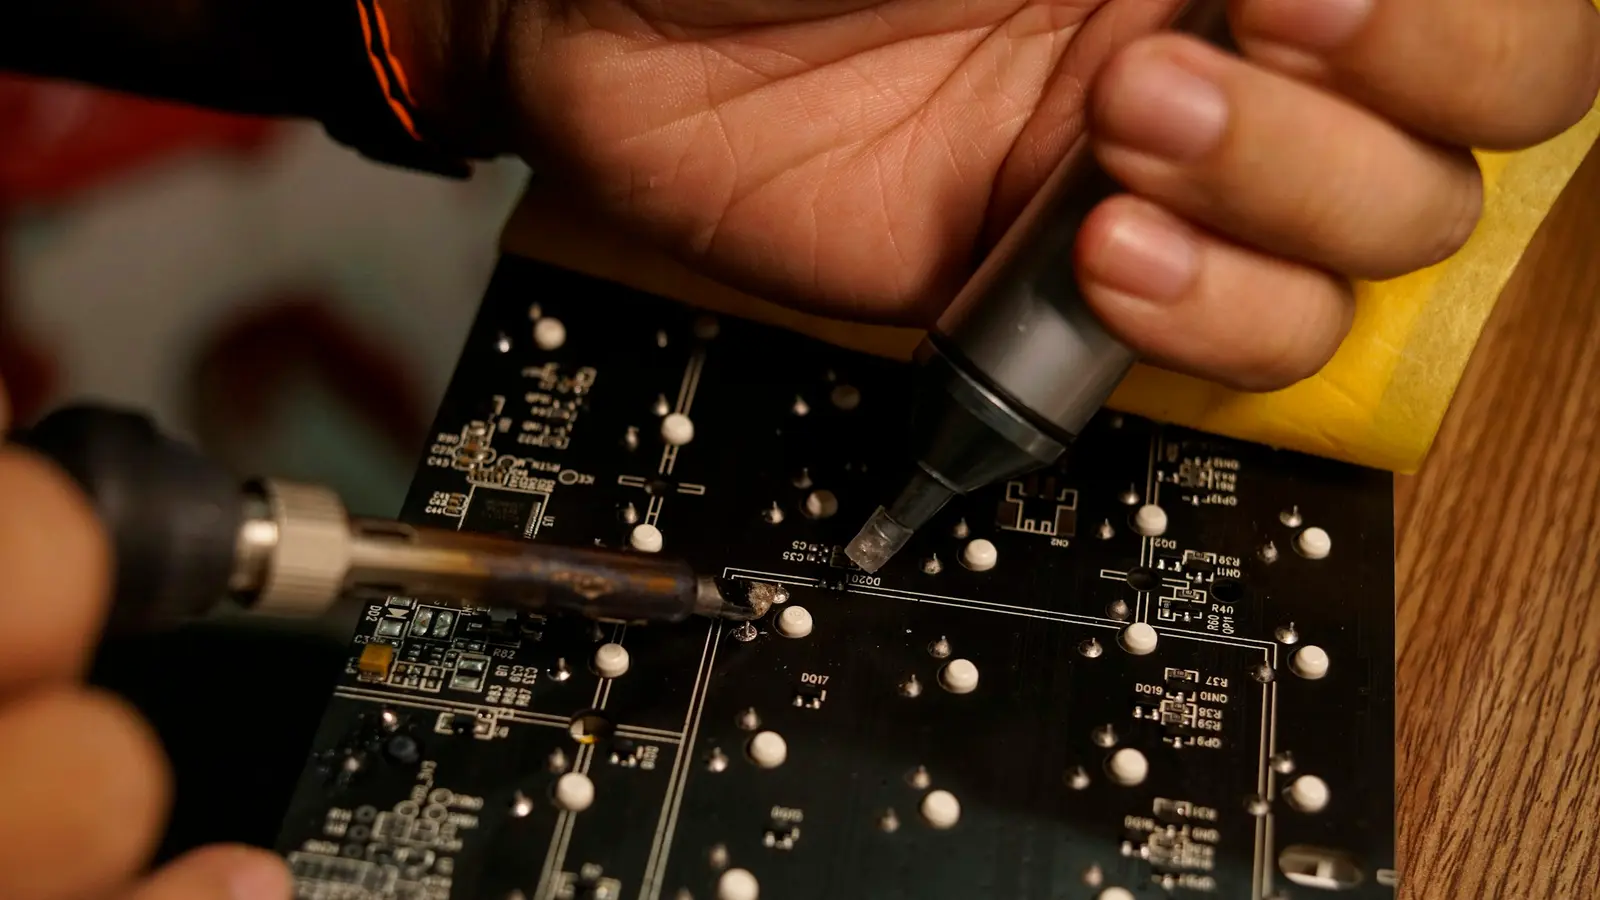
- Press the tip on the braid. Put the flat of the tip on top of the braid, directly over the solder. Heat passes through the copper into the joint. Do not scrub or press hard.
- Watch it wick. As the solder melts, it flows up into the braid, which turns silver. If solder remains, move to a fresh section and repeat.
- Lift together. Lift the braid and the iron away at the same time, while the solder is still molten. If the braid cools onto the pad and you pull it, you can tear the pad off the board.
- Trim. Cut off the used, silvered section so the next job starts with fresh braid.
- Clean up. Deal with flux residue according to the flux you used, as below.
When the wick won't work
| Symptom | Likely cause | Fix |
|---|---|---|
| Solder will not move into the braid | Not enough heat reaching the solder | A bigger or flatter tip, more flux, fresh braid |
| Braid stuck to the board | It cooled before you lifted it | Reheat the braid, then lift braid and iron together |
| Fine on small pads, fails on large ones | A ground plane is pulling heat away | A larger tip, a higher temperature, more flux and a longer dwell[7] |
| Joints that may be lead-free resist | Lead-free solder melts hotter and wets less readily | More heat and more flux[6][2] |
| Braid looks dull or dark | Old, oxidized braid | Cut back to a bright section and add flux |
Protect the pads
Adafruit describes a lifted pad as one that has come away from the board.[3] Three habits keep pads where they belong:
- Let heat, not pressure, do the work. Scrubbing with the braid can tear a pad loose.
- Lift the braid and the iron together, never the braid alone after it has cooled.
- When a joint will not give up its solder, stop and add flux or fit a bigger tip rather than holding the iron there longer and longer.
Cleaning up afterward
What comes next depends on the flux:
- No-clean: SparkFun says cleaning and flux removal are not required; isopropyl alcohol removes the residue if you want it gone.[1]
- Water-soluble: SparkFun says to remove any remaining residue from the board.[1]
- Rosin: Kester says rosin residues are normally non-conductive and non-corrosive, so removing them is cosmetic, unless the assembly works above 200 °F, where the residue melts, becomes conductive and must be removed.[8]
More in how to clean flux residue.
Next
Questions
Why won't my solder wick soak up solder?
Usually too little heat is reaching the solder through the braid, or there is too little flux. Add flux, move to a fresh section of braid and press a larger, tinned tip flat on top of the braid over the solder.
Should I use solder wick or a desoldering pump?
Use wick for flat jobs such as pads and bridges, and a pump to clear solder out of through-holes; SparkFun calls a solder vacuum a great tool for that job.[1]
Do I need extra flux if the braid is already fluxed?
It often helps. iFixit notes that braid usually has dry flux applied, but adding a little fresh flux to the joint is the first thing to try when the braid won't take solder.[2]
What width of solder wick should I buy?
Pick braid about as wide as the pads you clear most often. A narrow roll for fine-pitch surface-mount work and a wider one for through-hole pads covers most benches.
Can solder wick lift a pad?
Yes, if braid that has cooled onto the pad is pulled away, or if you scrub with it under pressure. Lift the braid and iron together while the solder is still molten; Adafruit describes a lifted pad as one that has come away from the board.[3]